Veneered Plywood sits at the intersection of appearance, strength, and material efficiency. Buyers use it for furniture, cabinetry, doors, and interior panels, where a clean surface and stable core both matter. Yet the product name alone says little about quality. Veneer species, thickness, core construction, bonding, sanding, and finish can vary substantially between suppliers.
Industry data offers useful context, but not a complete buying guide. The UNECE/FAO Forest Products Annual Market Review tracks developments across wood-based panels and related forest products. FAOSTAT’s Forestry Production and Trade database provides production and trade statistics, although product categories may not isolate every veneered-plywood grade. Read the figures carefully. They show market activity, not whether a specific factory will meet your tolerances or delivery schedule.
That distinction shapes this guide to the Top 10 Veneered Plywood Manufacturers for Global Buyers. It considers product range, manufacturing capability, export experience, certifications, and the clarity of technical documentation. Buyers should still request current test reports, sample panels, and written specifications before placing an order. A sample can look convincing under showroom lighting. It may behave differently after machining or finishing. No shortlist removes that risk, and supplier information can change. Use these profiles as a starting point, then verify each claim directly with the manufacturer.
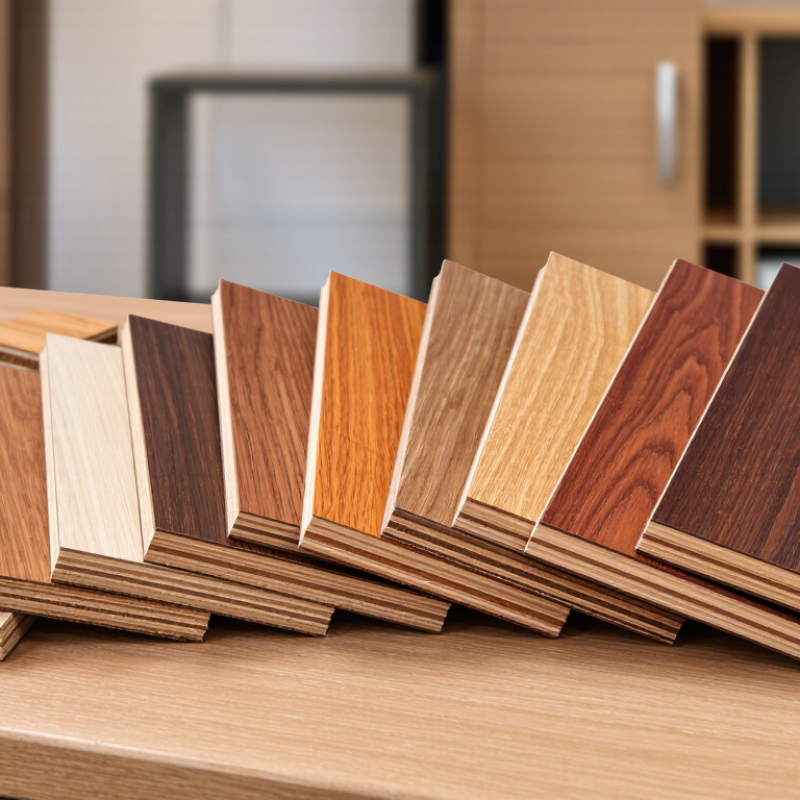
Veneered plywood combines thin wood faces with a layered core. The face veneer affects appearance, sanding, and finishing, while the core contributes stiffness and stability. Species and veneer grade can change the look considerably, even between panels sold for similar uses. At a cut edge, check for gaps, overlaps, or uneven layers. Looks matter. So does balance.
EN 636 classifies plywood by intended conditions of use. EN 636-1 covers dry conditions, such as heated interiors. EN 636-2 addresses humid conditions, including some protected spaces with variable moisture. EN 636-3 is intended for exterior conditions. These classes help buyers compare products, but they do not replace project-specific assessment. Exposure, edge details, bonding, and installation all matter. A panel suitable for exterior conditions is not automatically right for every outdoor application.
For international sourcing, request the technical data sheet and confirm the declared EN 636 class, thickness, and face grade. Check whether the panel needs sealing or protective finishing, especially at edges and cut-outs. A common oversight is judging a sheet by its face alone. I would not do that. One attractive surface can hide a core that does not match the job.
When comparing ten global veneered plywood manufacturers, assess capacity, export performance, and product grades using verifiable evidence. Ask for monthly production figures, typical lead times, and recent shipment records. A large factory may still run near capacity, leaving little room for urgent orders. Numbers need context. Check whether quoted capacity reflects actual output or an ideal production schedule.
Tips: Request samples from the same grade and thickness you plan to buy. Inspect veneer matching, surface repairs, edge finish, and thickness consistency. Ask how grades are defined, since labels can vary between suppliers. Keep written specifications for a fair comparison.
Export experience matters beyond destination lists. Ask about packing methods, shipment frequency, and how the supplier handles damaged panels or delayed production. Compare face veneer species, core construction, adhesive details, and available quality reports. If possible, test samples with your own requirements before placing a large order. I would not rely on a single impressive sample; it may not represent routine production. A clear, repeated specification is more useful than a broad promise of “premium” quality.
For global buyers, EN 314-2 and EN 636 answer different questions. EN 314-2 defines plywood bonding classes: Class 1 for dry conditions, Class 2 for humid conditions, and Class 3 for exterior conditions. EN 636 sets plywood requirements for dry, humid, and exterior use. The classifications are related, but they are not interchangeable. A panel’s declared end use should match its bond test results and performance documentation.
The scale makes careful verification worthwhile. FAO’s Global Forest Products Facts and Figures 2023 reports roughly 400 million m³ of wood-based panels produced worldwide in 2022. Ask suppliers for test reports identifying the standard, class, panel thickness, and test conditions. Check that the paperwork matches the delivered batch; a certificate alone cannot confirm storage or handling. A tidy document trail helps. It is not the whole story.
Tips: For exterior projects, request evidence for EN 314-2 Class 3 bonding and EN 636-3 performance. Confirm intended exposure with the designer, especially where edges face rain. Inspect veneer gaps, repairs, and panel flatness on arrival. Small defects matter. I would still question any claim that says “weatherproof” without specifying test conditions and limits.
For global buyers, a decorative veneer tells only part of the story. The panel beneath it must also meet applicable emissions requirements. Under TSCA Title VI, the formaldehyde emission limit for hardwood plywood is 0.05 parts per million. This is a chamber-test result, not a reading of indoor air in a finished room. A smooth surface or low-odor sample cannot confirm compliance.
Ask suppliers for current test and certification records that identify the product category, manufacturing site, and production period. Check that labels and shipping documents match the panels you receive. For a shipment of thin veneer-faced sheets, even a small mismatch in thickness or construction can raise questions about whether the paperwork covers that exact product. Details matter.
Keep the records. Really. Independent certification and recognized test methods provide stronger evidence than a general statement that a product is “low emission.” Requirements and documentation can change, so buyers should verify current rules with qualified compliance professionals. There is no perfect shortcut here: careful checks take time, and paperwork can still be confusing. Still, confirming the 0.05 ppm limit before purchase helps reduce avoidable sourcing problems.
For global buyers, a chain-of-custody certificate is a starting point, not a complete product check. Confirm that the certificate is current, covers the relevant product category, and matches the supplier’s legal entity. Check its status in the certification scheme’s public database. Then compare the invoice, packing list, and product claim. Names and reference numbers should agree. Small mismatches deserve questions.
Ask how veneer and core materials are tracked from receipt through pressing and packing. A clear batch code should connect the panels in your shipment to production records and supporting documents. Keep the records. If a supplier cannot explain how mixed sources are controlled, pause before relying on a logo or certificate alone. Paperwork can look reassuring. It can also be incomplete.
Batch testing adds another layer of evidence. Agree on the test method and acceptance limits before production, then sample panels from the actual lot, not a convenient showroom sheet. Depending on the application, check formaldehyde emissions, bonding performance, moisture, and veneer thickness. Request dated results identifying the batch and laboratory. For a higher-risk order, consider independent sampling and retain sealed reference pieces. One test cannot prove every panel is consistent; it is a useful snapshot, not a guarantee. Even careful checks can miss variation, so document what remains uncertain.
| No. | Due Diligence Dimension | What to Verify | Evidence or Reference | Buyer Check |
|---|---|---|---|---|
| 1 | FSC Chain of Custody | Confirm that the supplier’s certificate is valid and its scope covers the relevant product category and activities. Check that the specific order carries an eligible FSC claim. | FSC Chain of Custody requirements are set out in FSC-STD-40-004. Verify certificate details in the official FSC certificate database. | Match the certificate holder, scope, product description, and certificate status to the order documents. A certificate alone does not prove that every shipment is FSC-certified. |
| 2 | PEFC Chain of Custody | Confirm that the supplier holds a current PEFC-recognised chain-of-custody certificate and can make the required PEFC claim for the supplied goods. | PEFC chain-of-custody requirements are specified in the PEFC ST 2002 standard. Check certificate status through PEFC’s official certificate search. | Check that the certificate scope and sales documents correspond to the product and claim. Do not treat a certificate as proof of a claim on an unrelated shipment. |
| 3 | Transaction Documents and Claims | Ensure the purchase order, invoice, packing list, and shipping documents consistently identify the product and any certified-material claim. | Supplier certificate details, product descriptions, invoice claim, shipment records, and applicable certification rules. | Resolve differences in product names, quantities, certificate references, or claims before accepting the shipment. |
| 4 | Batch and Lot Traceability | Require a traceable link between each delivered batch and its production records, input materials, inspection results, and shipment. | Batch or lot codes; production dates; material issue records; inspection records; packing lists; and retained samples, where agreed. | Agree in advance how the lot code appears on panels, packaging, and documents, and how long records and samples will be retained. |
| 5 | Wood Species and Legal Sourcing | Confirm declared veneer and core species, country of harvest where available, and the documentation needed for the destination market. | Product specification, supplier sourcing records, applicable timber-legality documentation, and CITES documentation when a listed species is involved. | Check that species names and supporting documents are consistent. Legal and import requirements vary by jurisdiction and species. |
| 6 | Panel Construction and Veneer Quality | Specify face veneer species and grade, face thickness, core construction, panel thickness, dimensions, lay-up, and permitted defects. | Approved technical data sheet, purchase specification, agreed samples, and applicable product requirements such as EN 636 where relevant. | Define tolerances, repair limits, appearance criteria, and the inspection method in the contract rather than relying on a general product description. |
| 7 | Bond Quality and Intended Use | Match the adhesive and bond performance to the intended service conditions, such as dry, humid, or exterior use. | EN 314-2 provides bond-quality requirements for plywood; EN 636 specifies plywood requirements for different service conditions. | Request test reports for the specified construction and verify that the test classification is appropriate for the intended application. |
| 8 | Formaldehyde Emissions | Confirm the applicable emission limit and test method for the importing market and the specific panel product. | EN 717-1 is a chamber method for determining formaldehyde release. U.S. buyers should also check applicable TSCA Title VI requirements for regulated composite wood products. | Review reports for product identity, test method, result, laboratory, and date. Confirm whether the destination market requires additional documentation or labelling. |
| 9 | Mechanical and Physical Batch Testing | Set tests and acceptance limits for the properties relevant to the purchase, such as bending performance, dimensions, or moisture content. | EN 310 specifies a method for determining bending strength and modulus of elasticity of wood-based panels. Use the product specification to identify the required tests. | Agree sampling frequency, test method, acceptance criteria, and responsibility for independent testing before production begins. |
| 10 | Inspection, Nonconformity, and Corrective Action | Establish incoming inspection, defect classification, handling of failed tests, and a documented corrective-action process. | Contract inspection plan; inspection and test records; nonconformity reports; corrective-action records; and agreed independent inspection procedures. | Define remedies, retesting rules, and responsibility for rejected goods in the contract. Use a mutually agreed sampling plan; no single sample rate applies to every order. |
WhatsApp us